
RuboBTA Breakthrough Curve
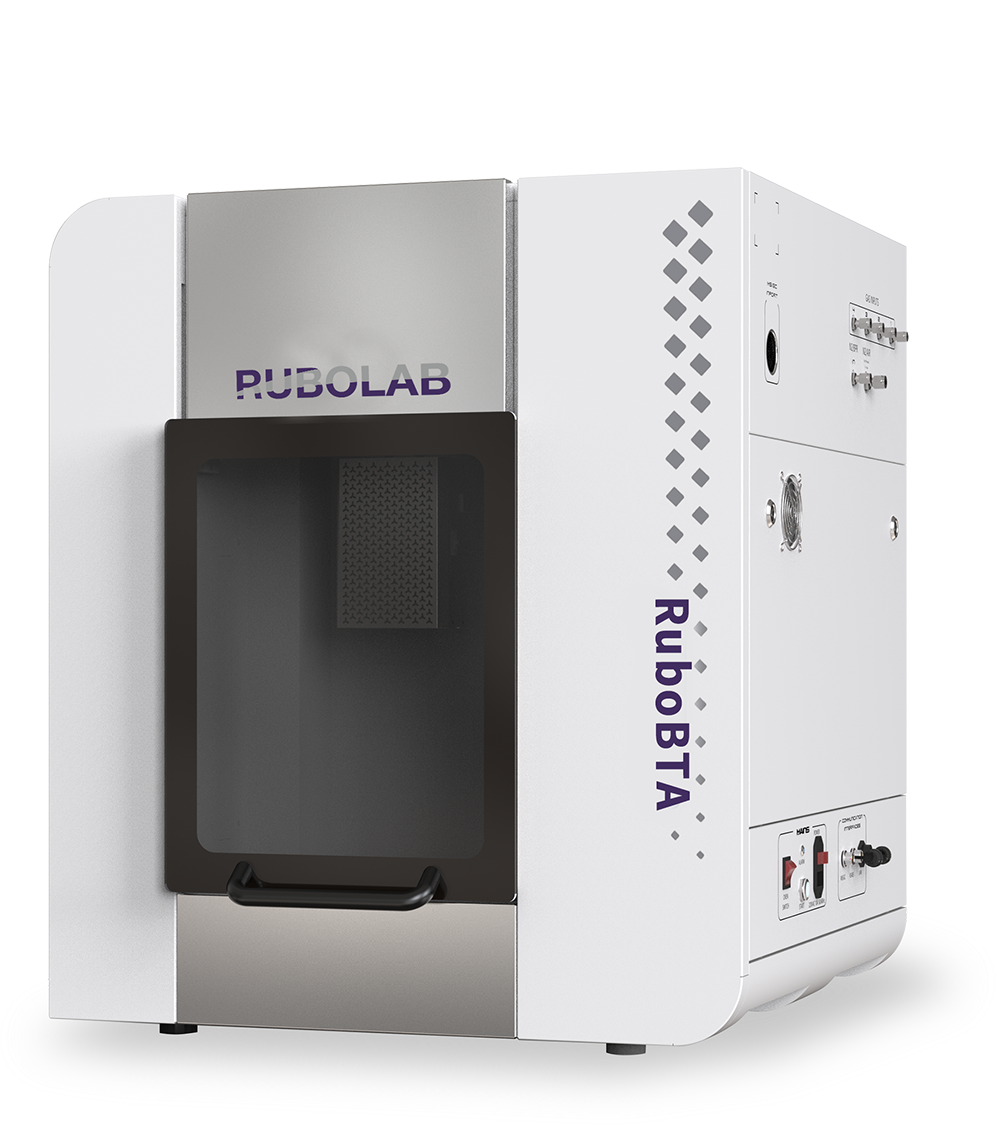
RuboBTA is a fully automatic dynamic adsorption analyzer integrating breakthrough curve testing, multi-component competitive adsorption, and mass transfer kinetics analysis. Using the dynamic flow method, it accurately simulates industrial adsorption–separation processes, providing critical data for adsorbent screening, process optimization, and mechanistic studies by deeply analyzing separation performance, competitive adsorption behavior, diffusion rates, and cyclic stability.
Core Functions
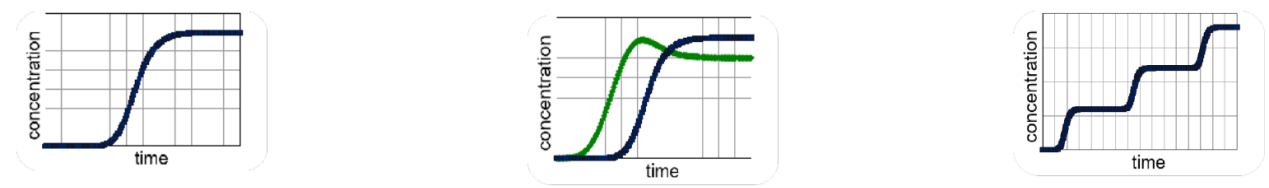
Basic Analysis: Precisely determines breakthrough time and adsorption capacity, evaluates selectivity in multi-component competitive adsorption, measures dynamic adsorption isotherms, and investigates adsorption kinetics.
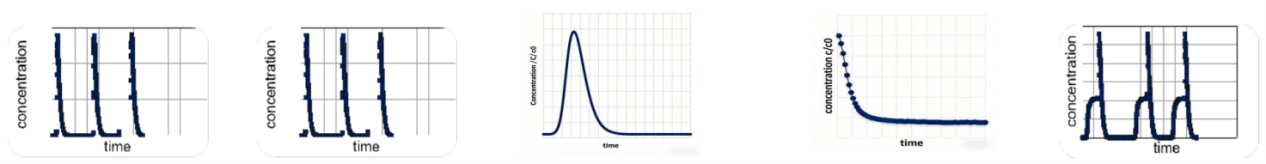
Process Simulation: Supports adsorption–desorption cyclic stability testing, Temperature Swing Adsorption (TSA), Pressure Swing Adsorption (PSA), Zero-Length Column (ZLC) method, and chromatographic diffusion coefficient determination.
Advanced Options (Optional): Offers vapor adsorption (bubbler-type vapor generator for organic vapors), corrosive gas adsorption (corrosion-resistant gas lines for SO₂, H₂S), carrier-gas-free operation (direct MS coupling), membrane separation and liquid adsorption modules, and in-situ adsorption/XRD combination module.
Mechanism Studies: Built-in competitive adsorption simulation, real-time monitoring of heat and temperature changes during adsorption, and intelligent interpretation of complex mass transfer processes.
Key Features
Flexibility & Efficiency: Independent main and bypass gas paths, standard 6 MFCs, supporting multi-adsorptive switching and online mixing. Compatible gases include H₂, N₂, CO₂, CH₄, C₂H₄, C₃H₆, n-C₄H₁₀, and corrosive gases at <1% concentration. Flow ranges: 0.2–10 mL/min or 1–50 mL/min, accuracy ±0.5% Rd + ±0.1% FS, pressure rating ≥10 bar, FFKM seals, response <2 s. Optional up to 2 independent vapor sources (–10 to 90℃), valve oven up to 120℃, supporting 0–90% relative humidity and organic vapors like methanol, ethanol, and benzene.Compressed air is used to drive pneumatic valves.
One instrument integrates breakthrough curves, competitive adsorption, PSA/TSA, and diffusion coefficient measurement, with upgradable options for membrane separation, liquid adsorption, and in-situ XRD, avoiding redundant investment.
Accuracy & Reliability: Automatic pressure control (atmospheric to 10 bar, accuracy 0.1 bar), high-precision TCD detector (≥63℃, noise <1% F.S.), back-pressure valve control accuracy ±0.25% FS. Full-line thermostatic valve oven (room temperature to 120℃) eliminates cold spots. Temperature control via circulating bath (–10 to 90℃, accuracy ±0.05℃), heating jacket, and furnace, covering –10 to 400℃ (optionally up to 1000℃) with linear heating ≥10℃/min. All-metal sealed corrosion-resistant gas paths ensure safe testing of SO₂, H₂S, and other corrosive gases.
Intelligent & Easy-to-Use: Software provides standard experimental protocols and fully automatic operation (from in-situ pretreatment to analysis) with one-click start, minimizing manual intervention.
Comprehensive Safety: Equipped with safety shield, overpressure relief valve, combustible gas alarm, dual over-temperature protection, and smart work-area lighting. Software integrates gas alarms and automatic shutdown upon limit exceedance. Adsorber reactor equipped with burst disc to prevent sample blow-out.
Intelligent Software Suite
Real-time control of flow, temperature, pressure, valves, and detector signals; minimum data acquisition interval 1 s.
Seamless MS connection for synchronized data acquisition and automatic calibration.
Test process traceability with video playback.
Preset saturation vapor pressure parameters for ≥12 organic liquids, supports user-defined vapor types, and split-file saving for large datasets.
Data processing software delivers one-stop analysis of breakthrough curves, adsorption capacity, and diffusion coefficients, with one-click report generation.
Advanced simulation software integrates adsorption modeling, thermodynamic calculations, and competitive adsorption prediction.
Industry Applications
Suitable for energy, environmental catalysis, chemical separation, natural gas purification, and related fields.